CN
Phone:
19951065399
WHAT ARE YOU LOOKING FOR?
Dust collection in a shot blasting room does more than keep the enclosure cleaner. It helps operators see the workpiece, supports stable blasting conditions, reduces the amount of fine contamination circulating with reusable abrasive, and prevents excessive dust from spreading into surrounding production areas.
During blasting, the abrasive strikes rust, mill scale, old coatings, and the base material at high velocity. This creates a mixture of reusable abrasive, broken abrasive particles, coating debris, rust, and fine dust. If these materials are not removed effectively, visibility can fall quickly and the blasting process becomes harder to control.
For buyers comparing a shot blasting room for sale, dust collection therefore should not be treated as an optional accessory. The extraction system, filter arrangement, abrasive recovery system, room layout, and actual blasting workload need to work together as one process.
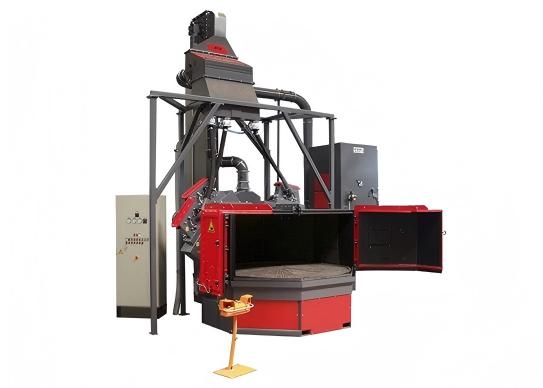
Dust in a shot blasting room comes from both the material being removed from the workpiece and the gradual breakdown of abrasive during repeated blasting cycles.
When abrasive strikes a steel surface, it removes contaminants that may include corrosion, mill scale, previous paint layers, and other surface residues. Some abrasive particles also fracture or wear down after repeated impacts, creating fines that should not remain mixed indefinitely with useful blasting media.
The amount and character of the dust can therefore change from one job to another. Removing light surface oxidation from newly fabricated steel does not create exactly the same dust load as stripping a thick aged coating from a large welded structure.
This matters when selecting dust collection equipment. A system should not be designed only around the physical dimensions of the blasting room. It also needs to reflect blasting intensity, the number of operators or nozzles working at the same time, abrasive type, workpiece condition, and expected production schedule.
Dust also interacts with the abrasive recovery process. Recovered material is rarely ready to return directly to blasting equipment. It needs to be separated so useful abrasive can continue through the cycle while dust and unsuitable fines are removed.
A well-designed blasting room therefore manages two related streams: airborne dust that needs to be extracted from the enclosure and recovered abrasive that needs to be cleaned before reuse.
Effective dust collection maintains visibility by continuously moving suspended fines away from the active blasting zone instead of allowing a dense dust cloud to build around the operator and workpiece.
Visibility has a direct influence on blasting efficiency. When an operator cannot clearly see the surface, it becomes more difficult to judge which areas have already been adequately blasted. The operator may pass over the same area repeatedly or miss recessed sections that still require treatment.
Both outcomes reduce process consistency.
A clearer working environment makes it easier to monitor changes in surface appearance as rust, scale, and coatings are removed. This is particularly important on large fabrications where operators move gradually across different faces, welds, corners, and structural details.
Good visibility also helps the operator position the nozzle more consistently. If the surface becomes obscured by airborne dust, controlling nozzle angle and working distance becomes more difficult, especially around complicated geometries.
However, simply installing a powerful exhaust fan does not guarantee good visibility. Dust needs to move in a predictable direction from the active blasting area toward extraction points. If air enters and leaves the room through poorly positioned openings, some areas can remain relatively clear while others develop persistent dust clouds.
This is why a buyer evaluating a shot blasting room for sale should look at the complete dust-control layout rather than comparing dust collector capacity in isolation.
Effective extraction requires enough airflow to capture suspended dust while maintaining a controlled air path across the blasting area and toward the dust collector.
The location of extraction points has a strong influence on this air path. Dust should be encouraged to move away from the operator's primary working position instead of crossing repeatedly through the blasting zone.
Room geometry matters as well. A long booth used for structural steel may require a different extraction arrangement from a shorter room used for compact machinery components. Large workpieces can themselves obstruct airflow, creating sheltered areas behind plates, beams, or equipment frames.
For this reason, airflow design should consider the room when it is occupied, not only when it is empty.
| Design Factor | Poorly Controlled System | Well-Designed Dust Collection |
|---|---|---|
| Air movement | Dust circulates or forms stagnant clouds | Air moves toward planned extraction points |
| Operator visibility | Surface frequently becomes obscured | Workpiece remains easier to inspect |
| Abrasive condition | More fines remain in circulation | Dust and reusable abrasive are separated more effectively |
| Filter operation | Uneven or rapid loading may occur | Loading is more predictable and manageable |
| Blasting process | More rework and unnecessary blasting may occur | Surface treatment is easier to control consistently |
Air entering the room must also be considered. Extraction cannot work properly without replacement air. Uncontrolled make-up air through doors and gaps can create local turbulence and carry dust in unwanted directions.
The objective is therefore not simply maximum suction. It is controlled movement of contaminated air through the working area and toward the filtration system.
Dust collector performance depends not only on the filter media itself but also on how effectively accumulated dust is removed and how filter resistance changes during operation.
As filters capture fine particles, dust builds on their surfaces and increases resistance to airflow. If this loading is allowed to continue without effective cleaning, extraction performance can gradually decline even though the fan is still operating.
Pulse-cleaning systems are commonly used in industrial blasting dust collectors to dislodge accumulated material from filter cartridges. The removed dust can then fall into the collection section instead of remaining embedded on the filter surface.
Maintenance teams should pay attention to changes in booth visibility, suction performance, filter pressure condition, unusual dust leakage, and the volume of material being collected. These operational signs can reveal problems before they noticeably reduce blasting productivity.
Leaks around ducts and collector connections also deserve attention. A system may have sufficient fan capacity on paper but perform poorly if damaged ducting or poorly sealed connections reduce useful extraction from the room.
Filter replacement should therefore be based on condition and operating performance rather than a fixed calendar alone. Blasting frequency, surface contamination, abrasive condition, and coating removal workload can all change how quickly filters load.
For facilities running frequent blasting cycles, easy access to cartridges and dust collection points also affects maintenance efficiency. A dust collector that is difficult to inspect or service is more likely to operate for too long in a deteriorated condition.
Better dust control improves blasting efficiency by giving operators a clearer surface to work on while helping the abrasive recovery system return cleaner, more useful media to the blasting process.
The relationship between dust collection and productivity is often underestimated. When visibility is poor, operators tend to slow down, repeat passes, or stop blasting to confirm surface condition. These small interruptions can become significant when treating large structures.
Abrasive quality matters too. A recovery system should separate reusable blasting media from dust, debris, and fines before the abrasive returns to storage and blasting equipment. If too much contamination remains in circulation, blasting behavior becomes less predictable and the useful abrasive mixture gradually deteriorates.
Dust control also supports downstream coating operations. Shot blasting is usually performed to create a clean, suitably prepared surface before painting or another protective coating is applied. More consistent blasting makes inspection easier and reduces the chance that poorly prepared areas move into the next production stage.
This is particularly relevant when the blasting room forms part of a larger industrial finishing line. The goal is not simply to remove visible rust quickly. The blasting stage must deliver repeatable surface preparation at a rate that matches the painting process that follows.
JZJ designs blasting rooms with dust removal and abrasive recovery integrated into the overall equipment system. When evaluating a shot blasting room for sale, buyers should therefore provide information about workpiece dimensions, surface condition, blasting media, production volume, material handling, and the expected number of simultaneous blasting operations.
Projects with unusual workpieces or production requirements can also be discussed directly through the JZJ contact page before the room, abrasive recovery, and dust extraction configuration is finalized.
Dust collection should be considered part of the blasting process itself rather than an independent environmental accessory.
The system affects how clearly operators can see the workpiece, how reliably airborne fines leave the blasting zone, how well recovered abrasive is separated from contamination, and how consistently the surface can be prepared for the next coating stage.
When comparing a shot blasting room for sale, looking only at room dimensions, blasting guns, or total equipment power gives an incomplete picture. The airflow path, extraction arrangement, filter-cleaning method, abrasive recovery system, and maintenance accessibility are equally important to long-term operating performance.
A properly coordinated system helps the blasting room remain productive as dust loading changes from one project to another, while giving operators better control over surface preparation quality.
Blasting generates fine particles from rust, coatings, surface contaminants, and broken abrasive. Dust collection removes suspended material from the working area to improve visibility and support controlled blasting conditions.
Not necessarily. Collector capacity is only one factor. Extraction-point location, replacement air, room geometry, duct design, workpiece position, and filter condition all influence how effectively dust leaves the blasting zone.
Recovered abrasive can contain dust, debris, and worn particles. Effective separation removes unwanted material so suitable abrasive can return to the blasting cycle with more consistent operating characteristics.
Reduced visibility, weaker extraction, abnormal pressure conditions, dust leakage, and declining collector performance can indicate filter loading or other maintenance problems. Inspection should be based on actual operating condition.
Provide the workpiece size and material, surface condition, abrasive type, required production capacity, material-handling method, number of blasting nozzles or operators, available facility space, and any relevant environmental requirements.